Applications
Different materials require different cutting and grinding approaches. Explore workflows, common issues and matched tools.
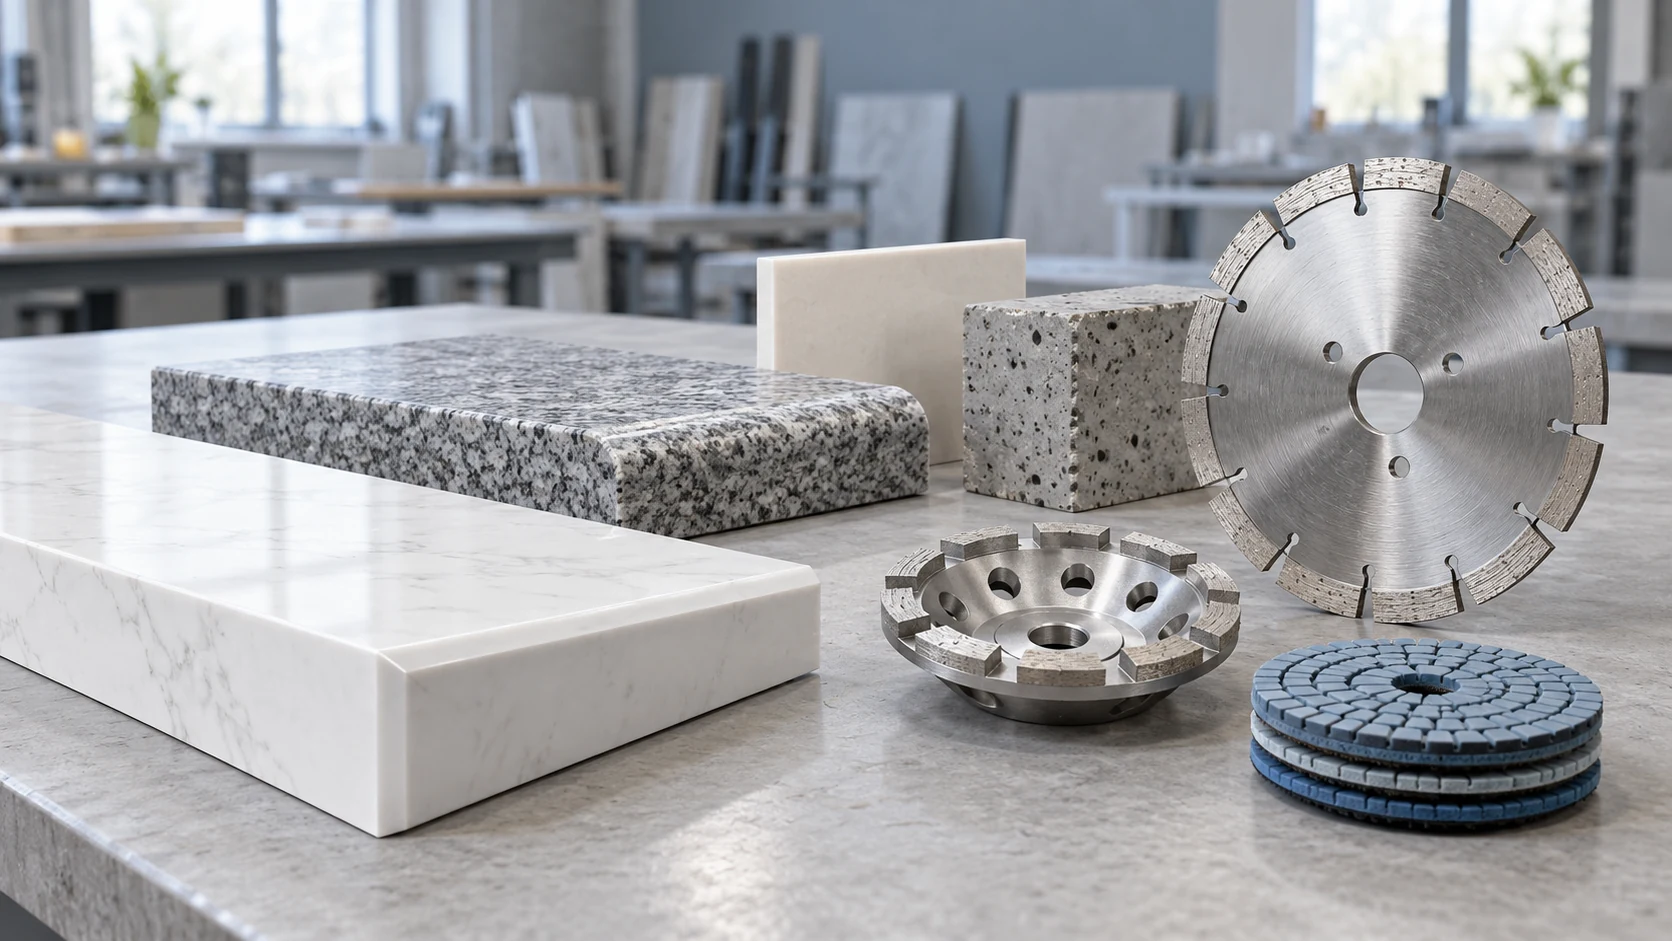
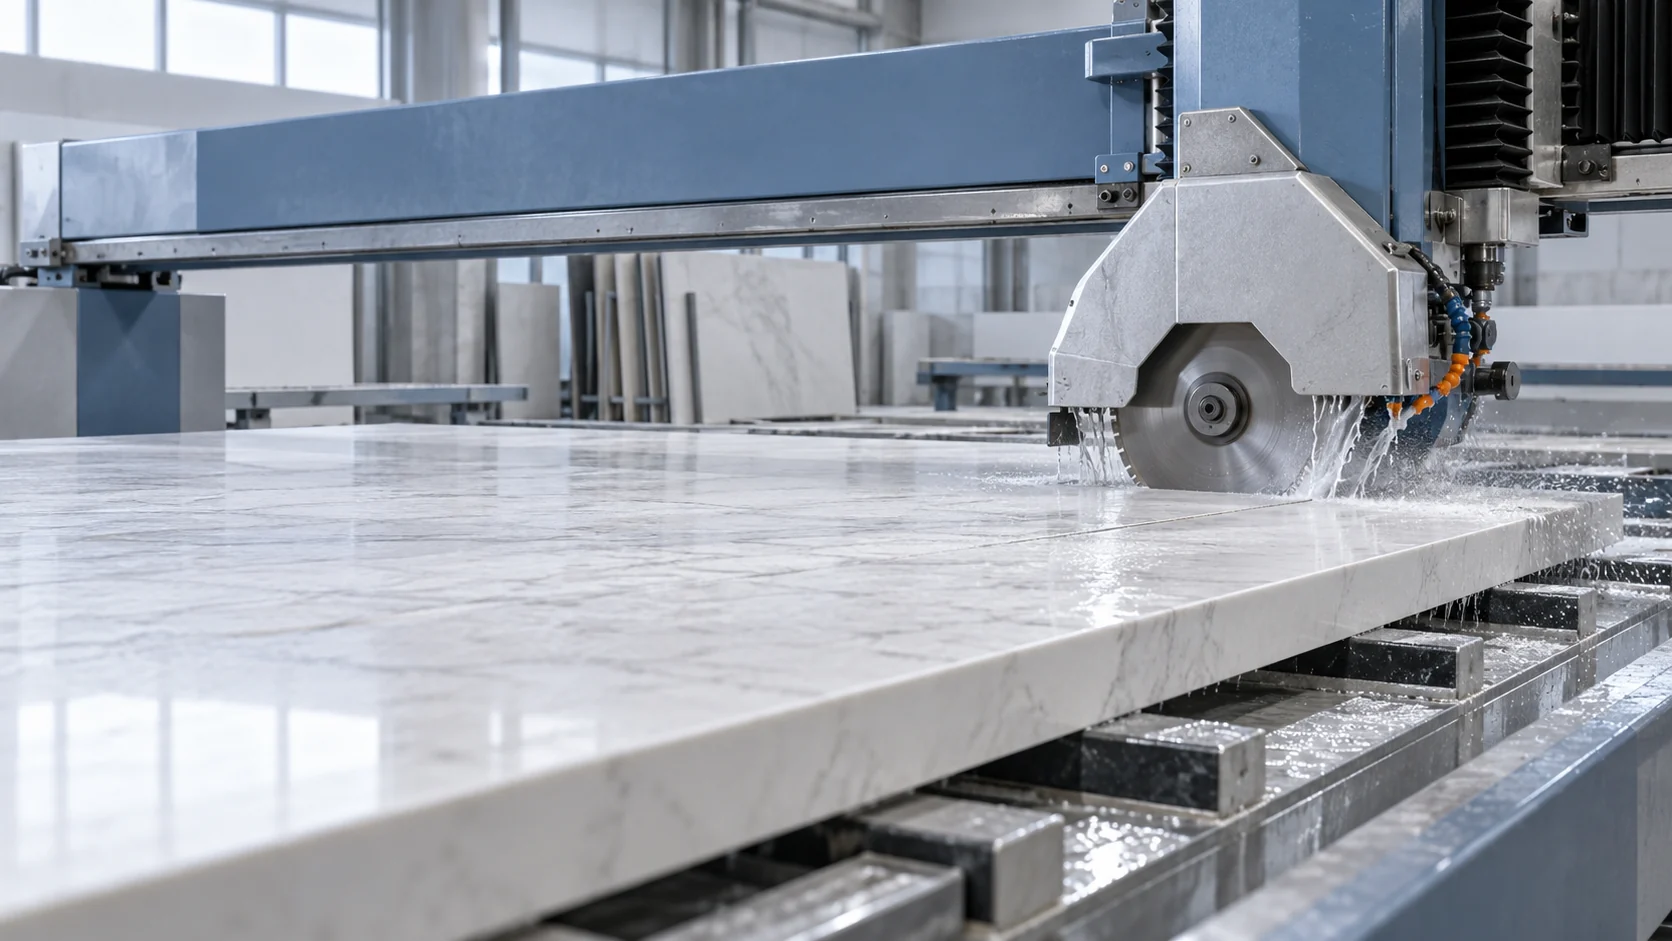
Sintered Stone & Quartz Countertop Fabrication
Granite & Marble Slabbing & Block Extraction
Concrete Road Sawing & Floor Grinding Prep
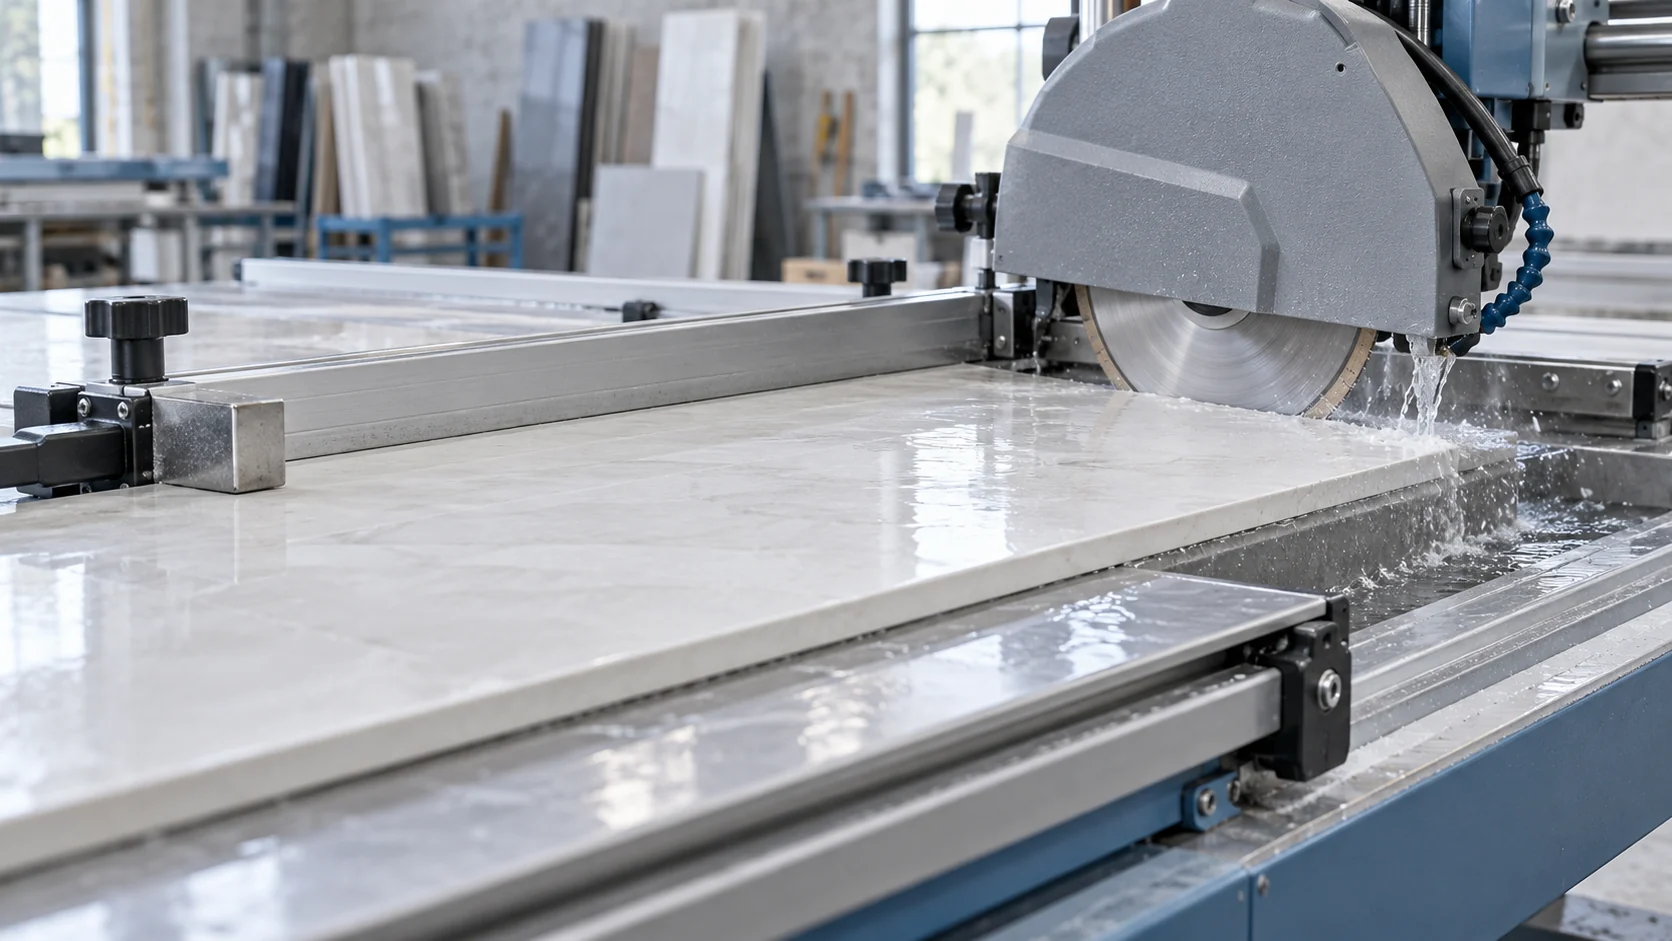
Ceramic & Porcelain Tile Precision Cutting
Sintered Stone & Quartz Countertop Fabrication
Complete tooling workflow: slab sizing, 45° waterfall miters, sink cutouts, and edge polishing.
Recommended Machining Workflow & Tooling Chain
Primary Slab Sizing
J-Slot Silent Blade QZ-SB-DK01
Note: Ensure abundant water flood; decelerate at entry/exit
45° Waterfall Mitering
V-Groove 90° Blade QZ-GV-V90
Note: Check machine rails and slab support; confirm feed against guidance and a trial cut
Faucet & Sink Hole Boring
Vacuum Brazed Wax Core Bit QZ-BZ-CB01
Note: Score lead crescent at 45°; never engage hammer mode
Edge Polishing & Touch-up
Dry Honeycomb Pads QZ-PP-DR07 (Step 1-3)
Note: Check pad markings and machine speed limits; progress through grits after a trial
Common Field Failures, Root Causes & Remedies
Diamond grit too coarse, matrix bond too hard causing glaze rubbing, or excessive axial runout causing radial vibration.
Switch to J-slot silent sintered stone blade with fine-grit matrix; dress on refractory brick; calibrate arbor flange clearance.
Tilting standard flat blades induces lateral flexing; excessive feed speed at the slab exit tears the brittle corner.
Consider the V-groove blade (QZ-GV-V90); set entry and exit feed against the machine and target-slab guidance, then trial-cut.
Using hammer drill mode or dry drilling without thermal relief; heavy vertical plunging jamming rock slurry.
Use vacuum brazed core bits with internal wax; tilt at 45° to start guide groove, then oscillate gently without percussion.
Operating Checklist to Confirm Before Ordering
To help match the tool to the job, prepare the following parameters:
- Slab thickness (e.g. 6mm wall facade / 12mm / 20mm countertop)
- Spindle motor power (kW) and current working RPM
- Current peripheral speed, tool-marked maximum RPM, and machine limits
- Current feed rate and trial adjustments against material and machine guidance
- Coolant water pressure and alignment directly onto the cut point
Matched Products in This Solution
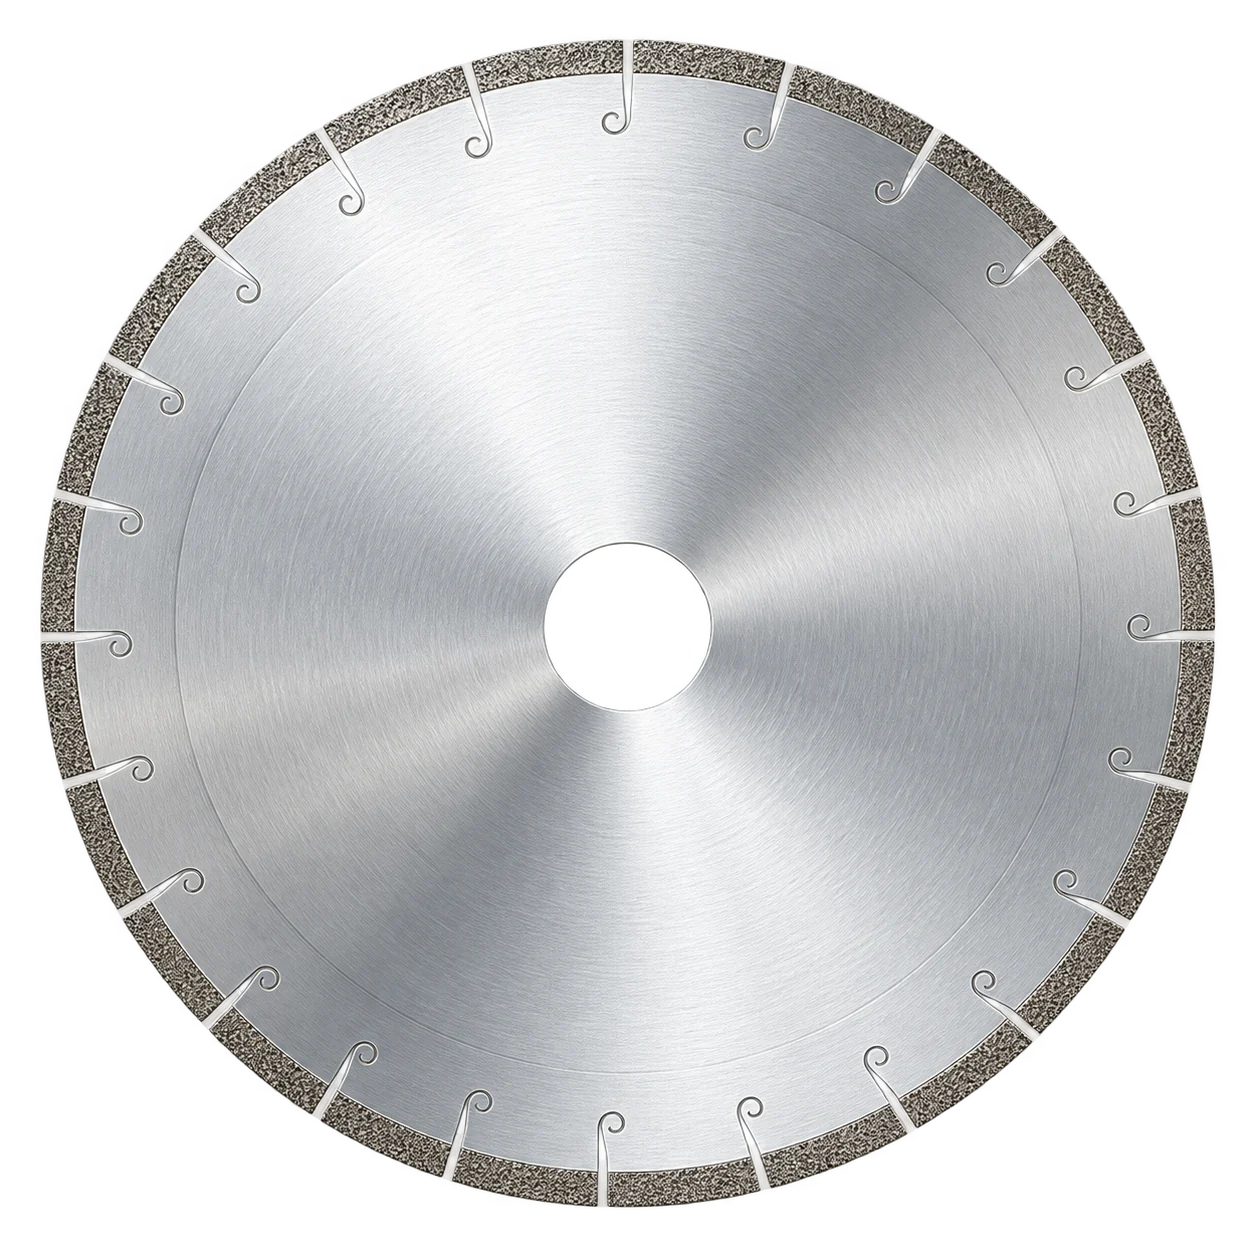
Diamond Blade For Dekton & Sintered Stone (J-Slot Silent)
Thin-segment blade listed for 3–20mm slabs; verify edge quality and wear in a trial cut on the target material.
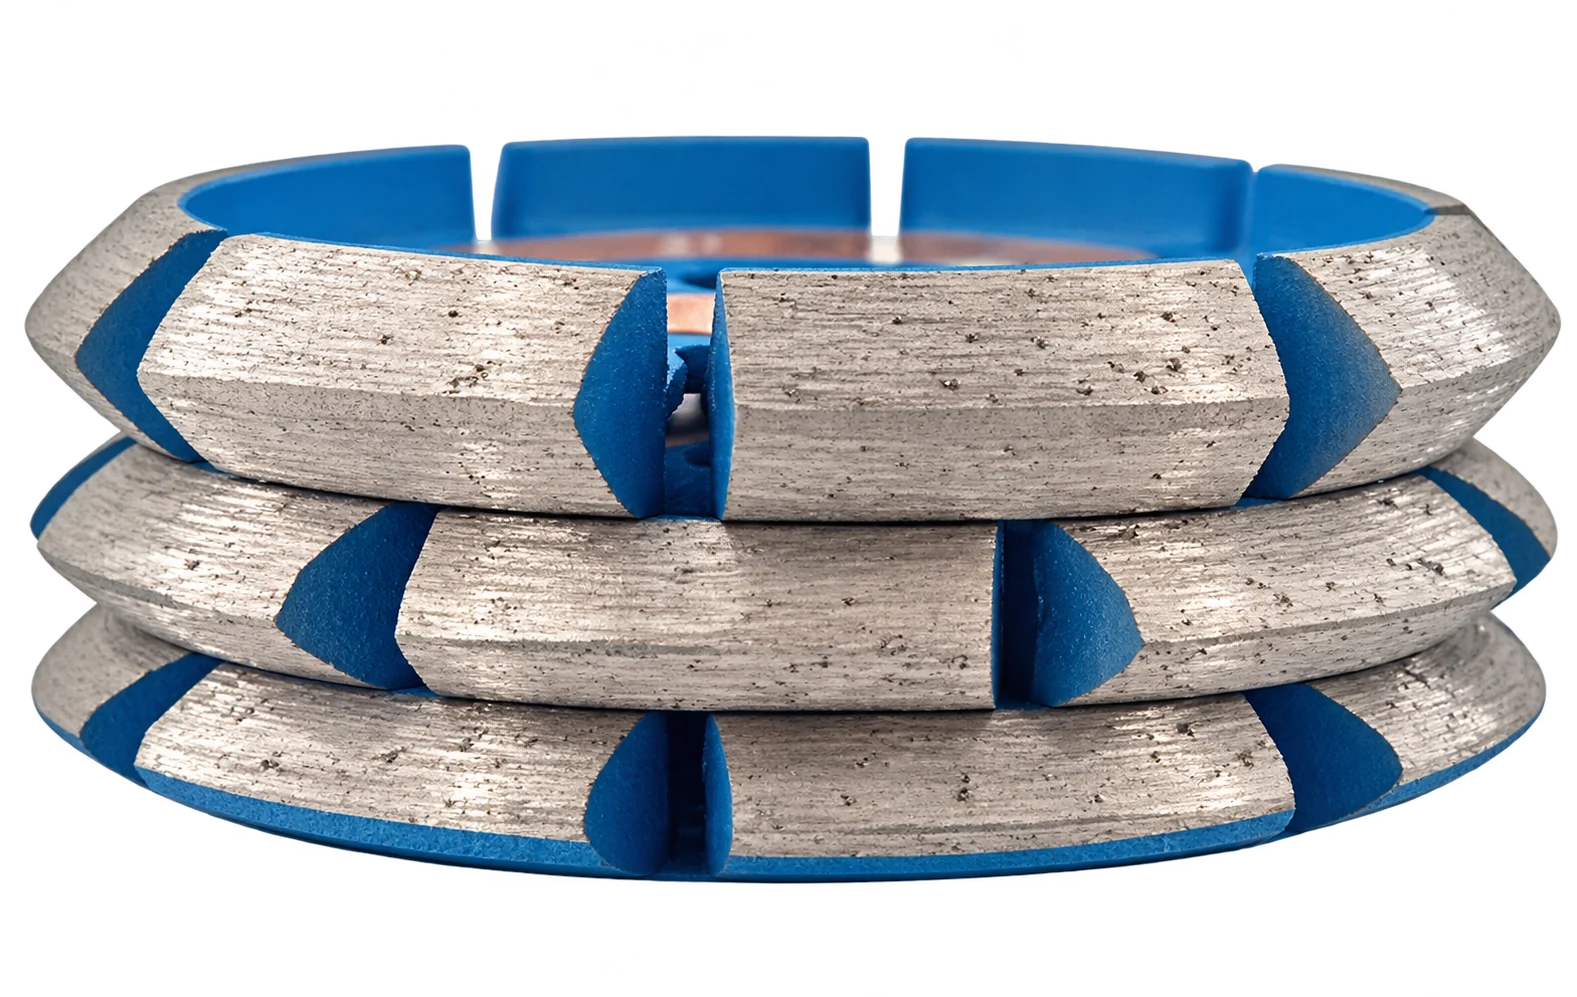
V-Shaped Slot Blade (90° Miter & Chamfer)
Application: Marble, Dekton, Ceramic. Diameters 110/125mm, thicknesses 6/8/10/15mm, arbor 20/22.23mm.
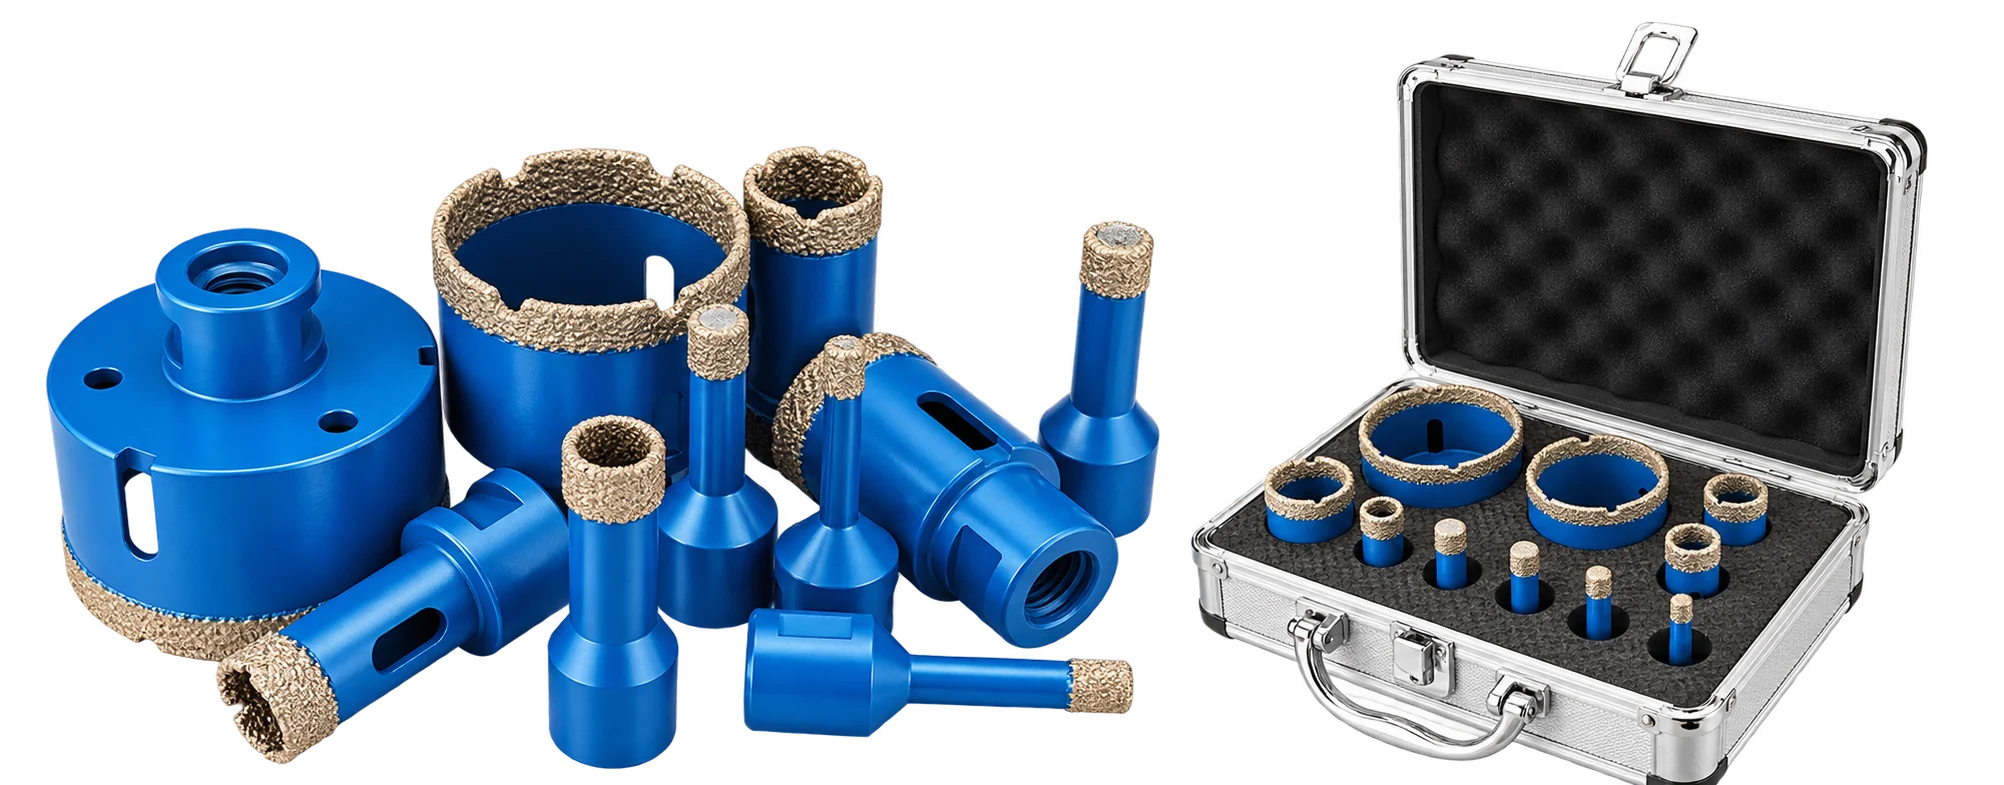
Vacuum Brazed Core Drill Bit & Finger Profile Bit
Wax-filled core bits for countertop drilling; confirm dry-use conditions, machine fitment and hole quality on the target material.
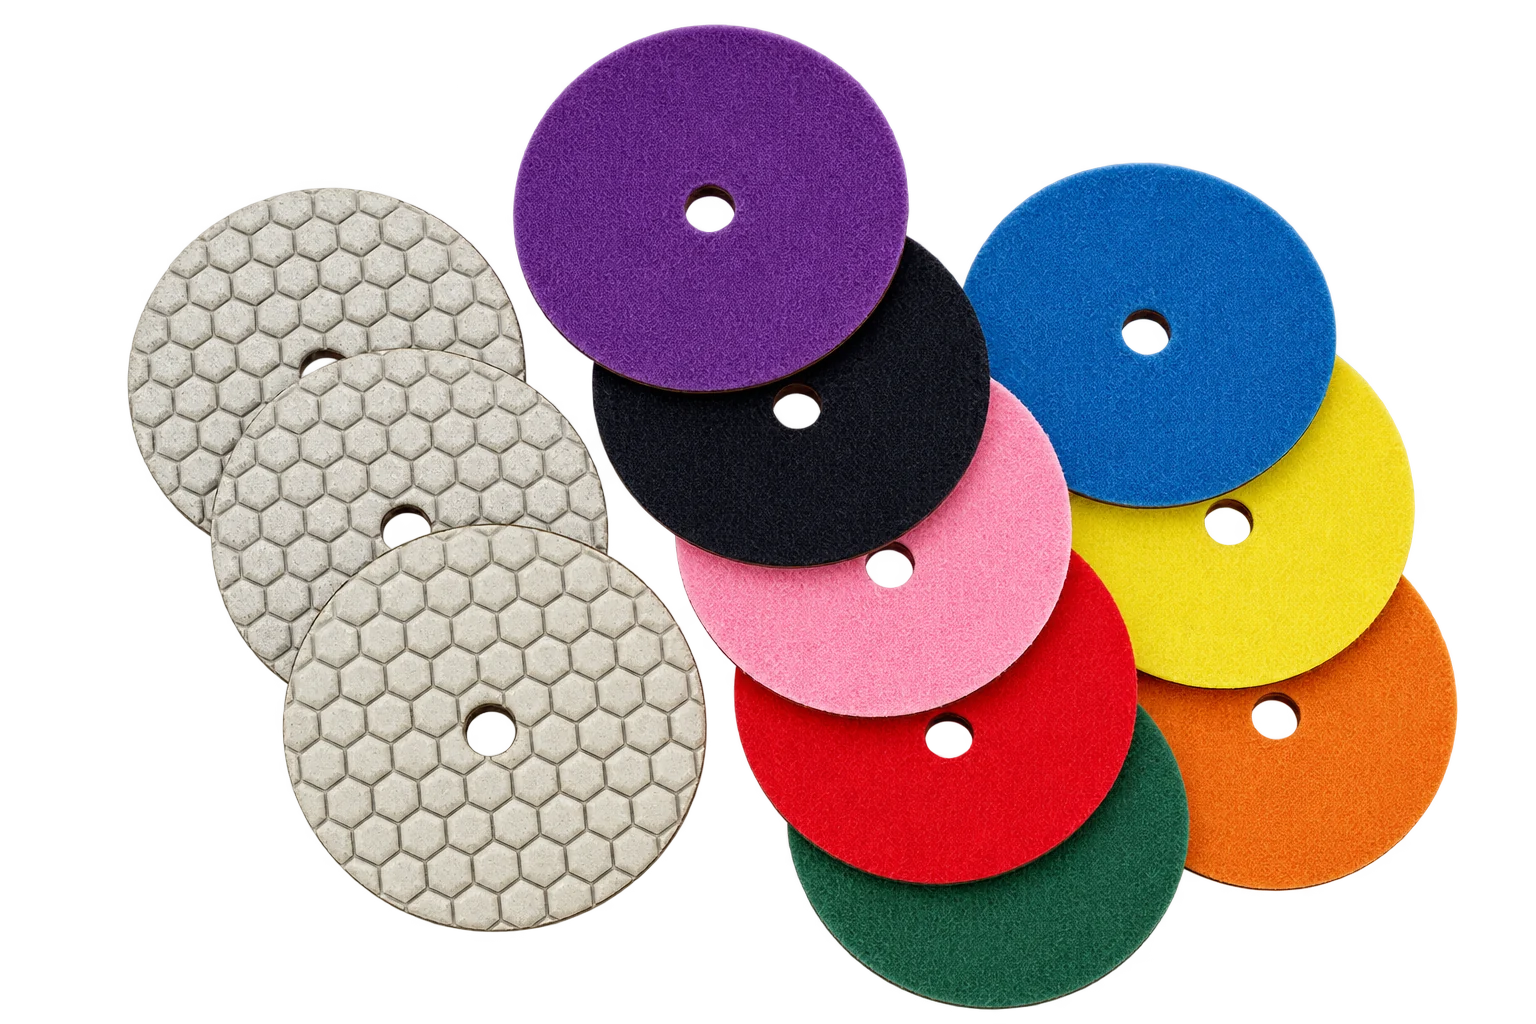
Diamond 7-Steps Dry Polishing Pad
Suitable for granite, marble, terrazzo, concrete, and artificial stone. Grits: 50#, 100#, 200#, 400#, 800#, 1500#, 3000#, BUFF.
Common Machining Bottlenecks & Engineered Remedies
Targeting real-world cutting and grinding challenges: edge chipping, floor tool glazing, block saw stalling, and OEM supply chain bottlenecks.
Edge Chipping & Corner Blowout on Sintered Stone Mitering
Micro-chipping and serrated spalling along cutlines or jagged 45° miter joints, causing high-value countertop slab rejections or tedious manual repairs.
Chipping may depend on the slab, blade condition, support, spindle runout, cooling, or feed. Record the defect location and check each factor.
- Check tool-marked maximum RPM and machine limits; record current peripheral speed
- Record straight and miter feed, then adjust in a trial against slab and machine guidance
- Inspect entry and exit chipping; adjust support and feed as needed
- Confirm coolant reaches the blade and workpiece contact zone
Diamond Blade For Dekton & Sintered Stone (J-Slot Silent)
Thin-segment blade listed for 3–20mm slabs; verify edge quality and wear in a trial cut on the target material.
Share your slab thickness, machine spindle RPM and power. We will review peripheral speeds and match trial specifications.