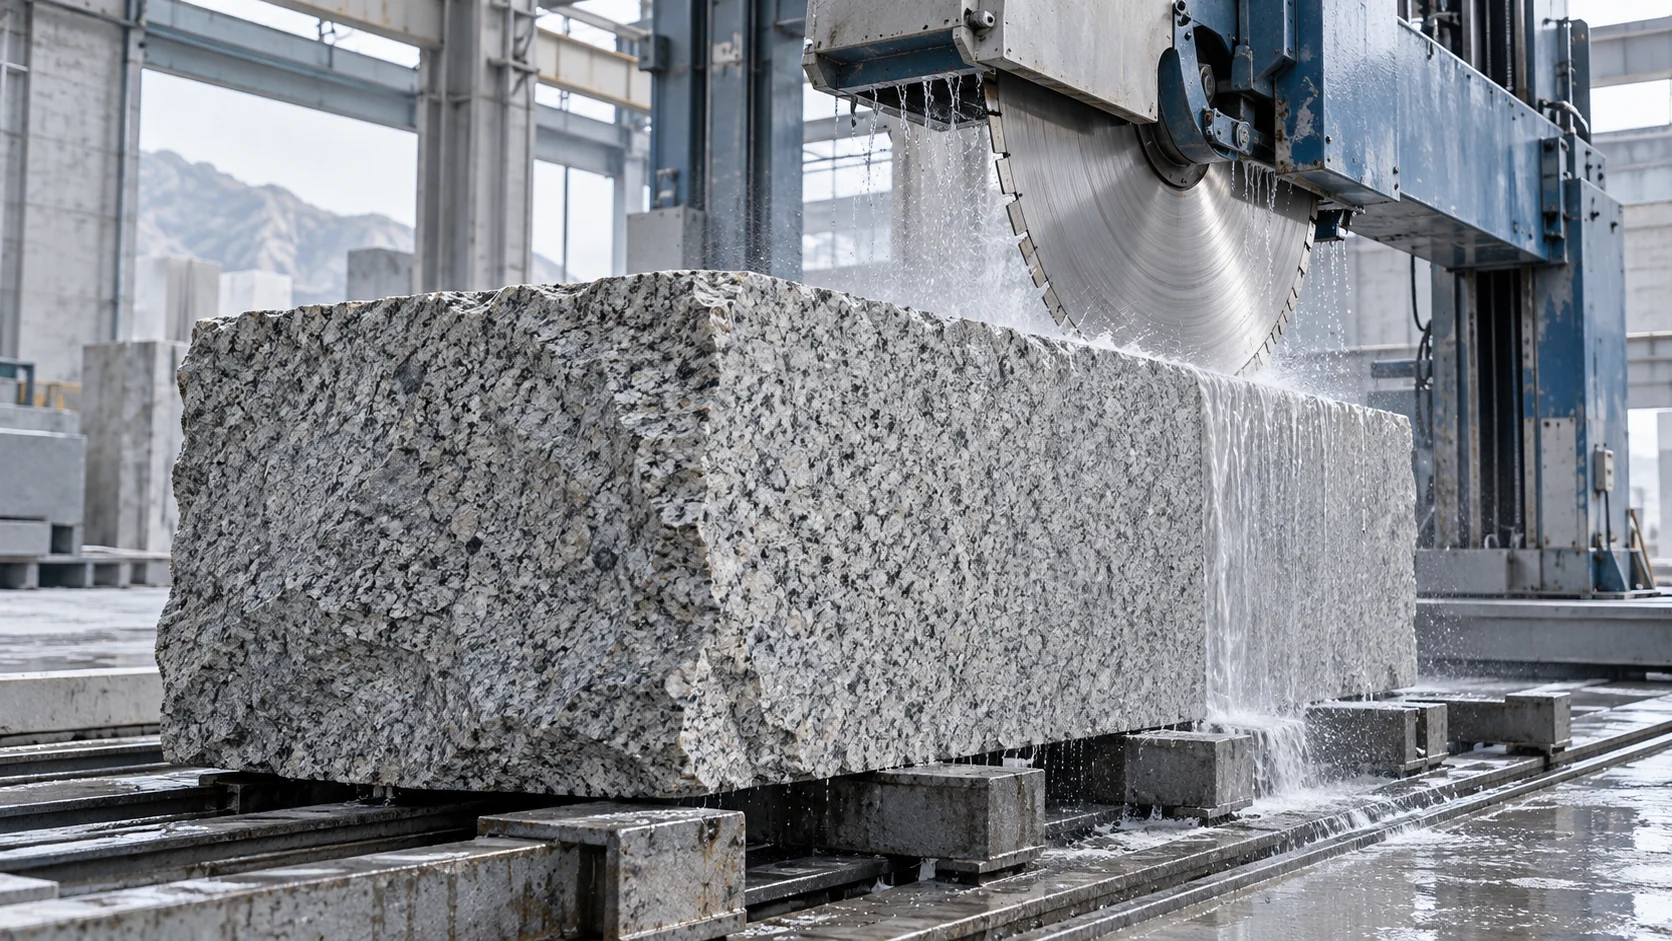
Granite & Marble Slabbing & Block Extraction
Specialized segment bond chemistry for high-quartz granite slabbing and crack-sensitive marble blocks.
Sintered Stone & Quartz Countertop Fabrication
Granite & Marble Slabbing & Block Extraction
Concrete Road Sawing & Floor Grinding Prep
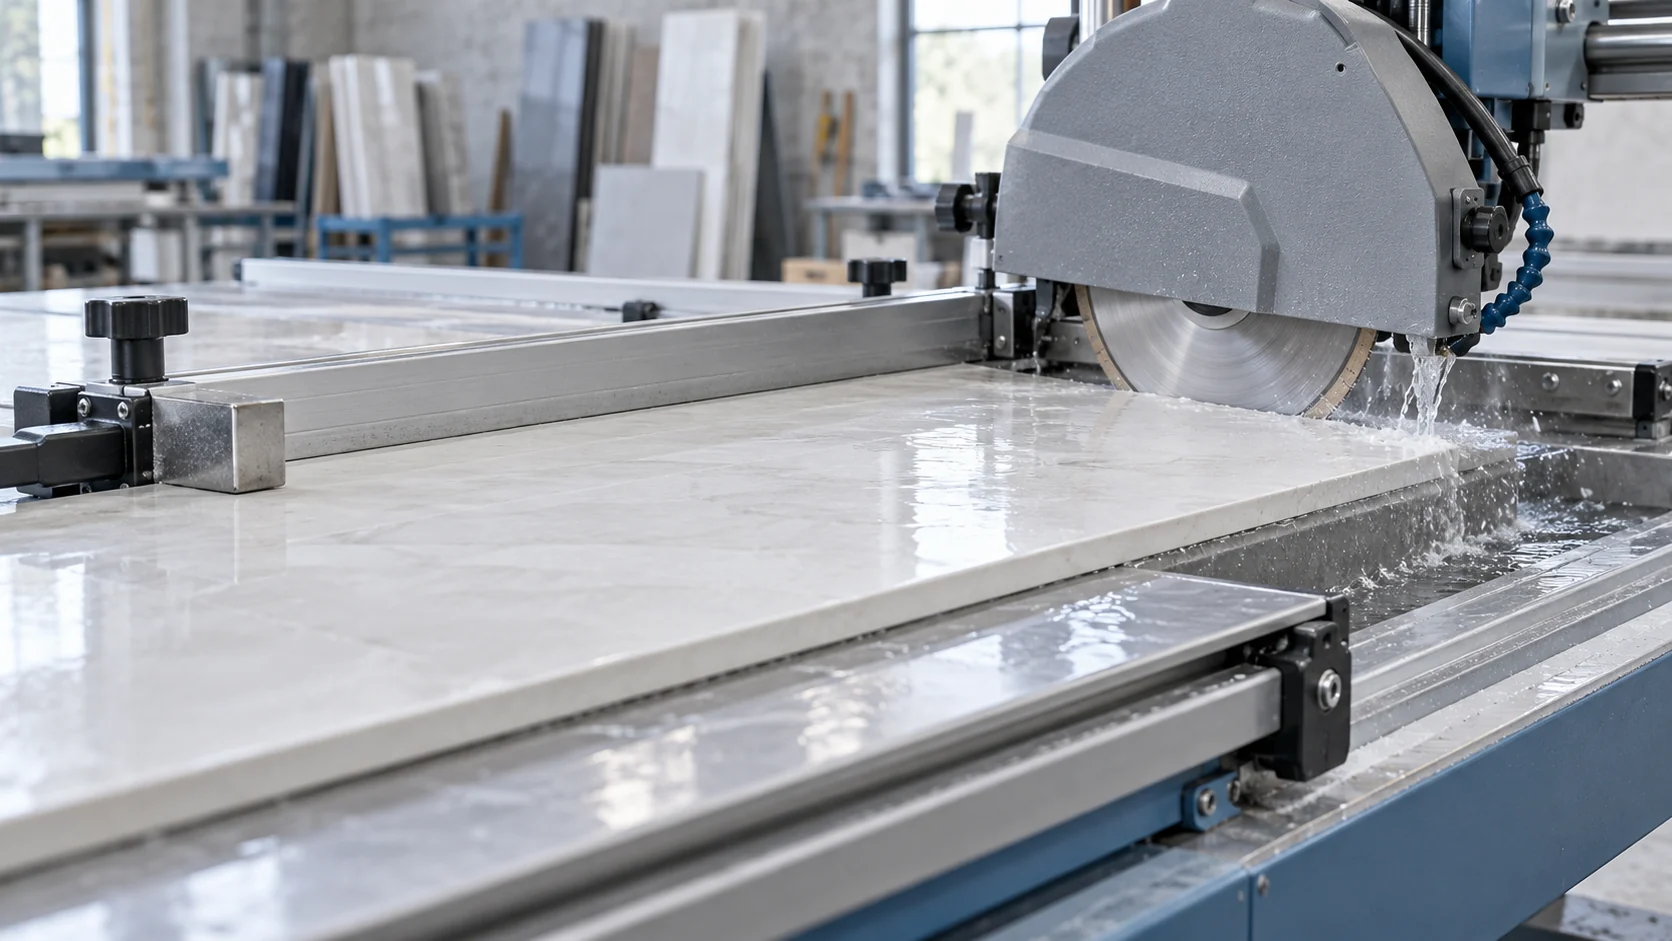
Ceramic & Porcelain Tile Precision Cutting
Granite & Marble Slabbing & Block Extraction
Specialized segment bond chemistry for high-quartz granite slabbing and crack-sensitive marble blocks.
Recommended Machining Workflow & Tooling Chain
Block Squaring & Positioning
Sandwich Segments QZ-SG-GR01 / Gang Saw Segments
Note: Maintain settling pond water cleanliness; moderate first cut depth
Slab Edge Trimming
Granite Silent Blade QZ-SB-GR01 / Marble Blade QZ-SB-MB01
Note: Confirm peripheral speed against the specific blade markings, machine data, and target-stone trial cut
Surface & Edge Wet Polishing
Wet Polishing Pads QZ-PP-WT06 (#50-#3000)
Note: Grind progressively; completely eliminate previous pass scratches
Common Field Failures, Root Causes & Remedies
Matrix bond is excessively hard for the specific granite; spent diamond crystals do not shed, causing thermal glazing.
Step down one matrix hardness grade; deploy M-shape sandwich multi-layer segments (QZ-SG-GR01).
Tension loss in the steel core; asymmetric segment side wear; uneven dual-side water manifold pressure.
Re-tension steel core and verify runout against specification; balance water jets symmetrically; specify rigid silent cores.
Operating Checklist to Confirm Before Ordering
To help match the tool to the job, prepare the following parameters:
- Stone quarry variety and quartz content (e.g., G654, Baltic Brown, Absolute Black, Carrara)
- Blade diameter and blade array (Single saw, Multi-blade gang array, Frame saw)
- Block dimensions, step-cut depth per pass, and traverse speed
- Spindle motor power rating and maximum operating amperage
Matched Products in This Solution
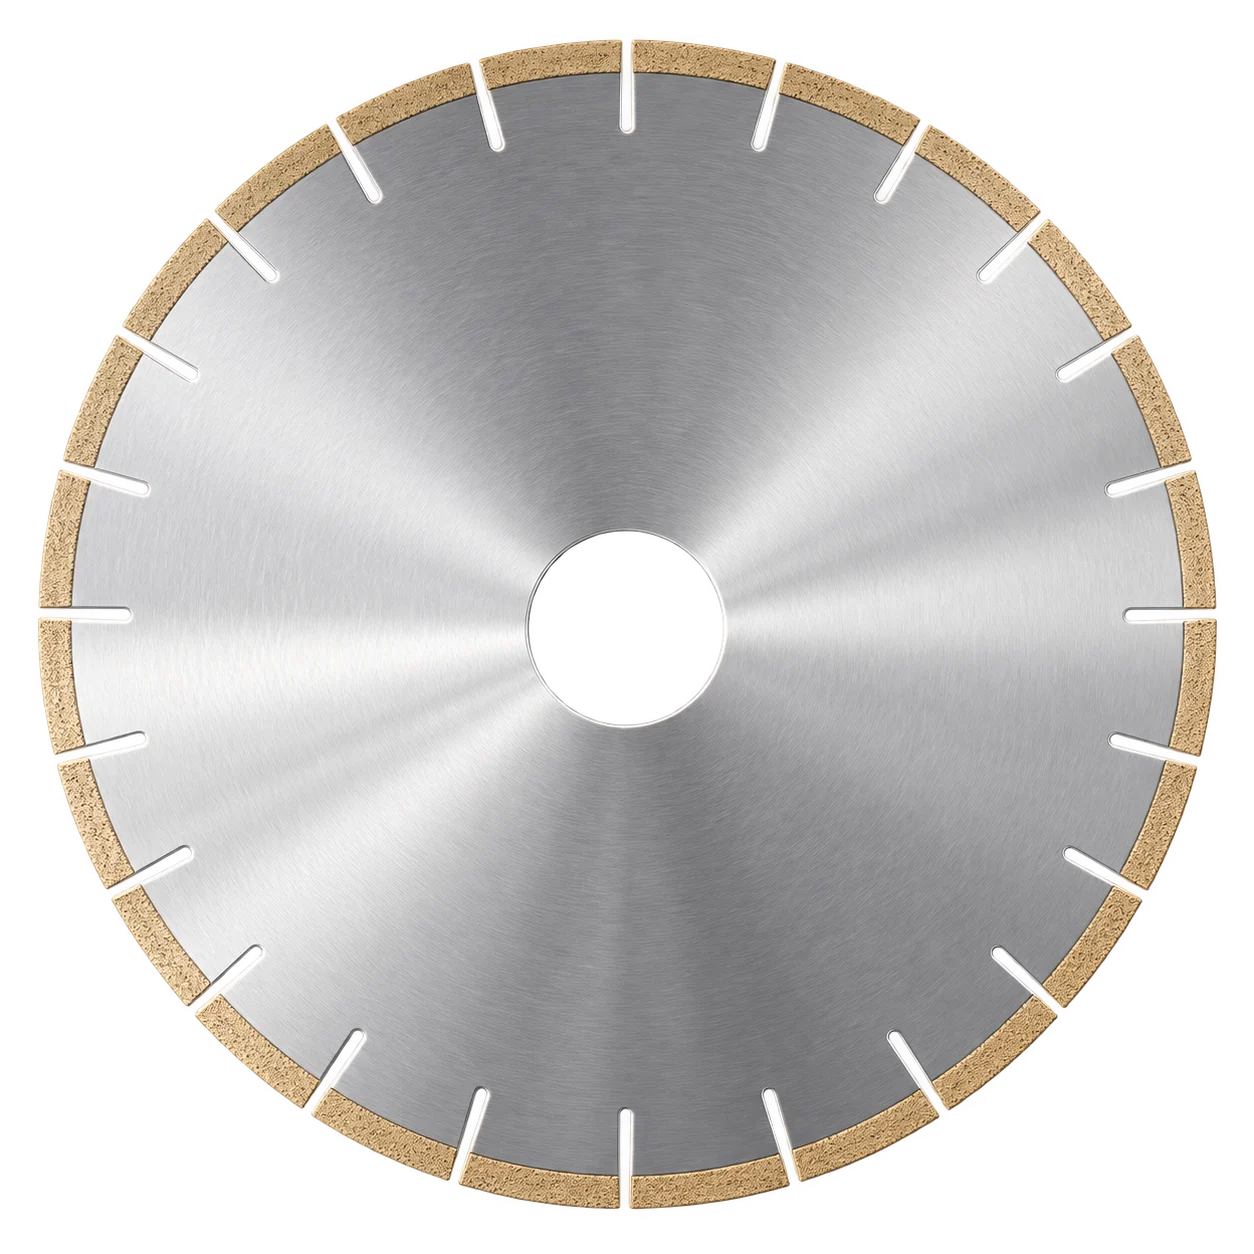
Diamond Blade For Marble (Straight Keyhole Slot)
Marble straight-slot blade with an optional damped core; verify cut quality and wear on the target slab and machine.
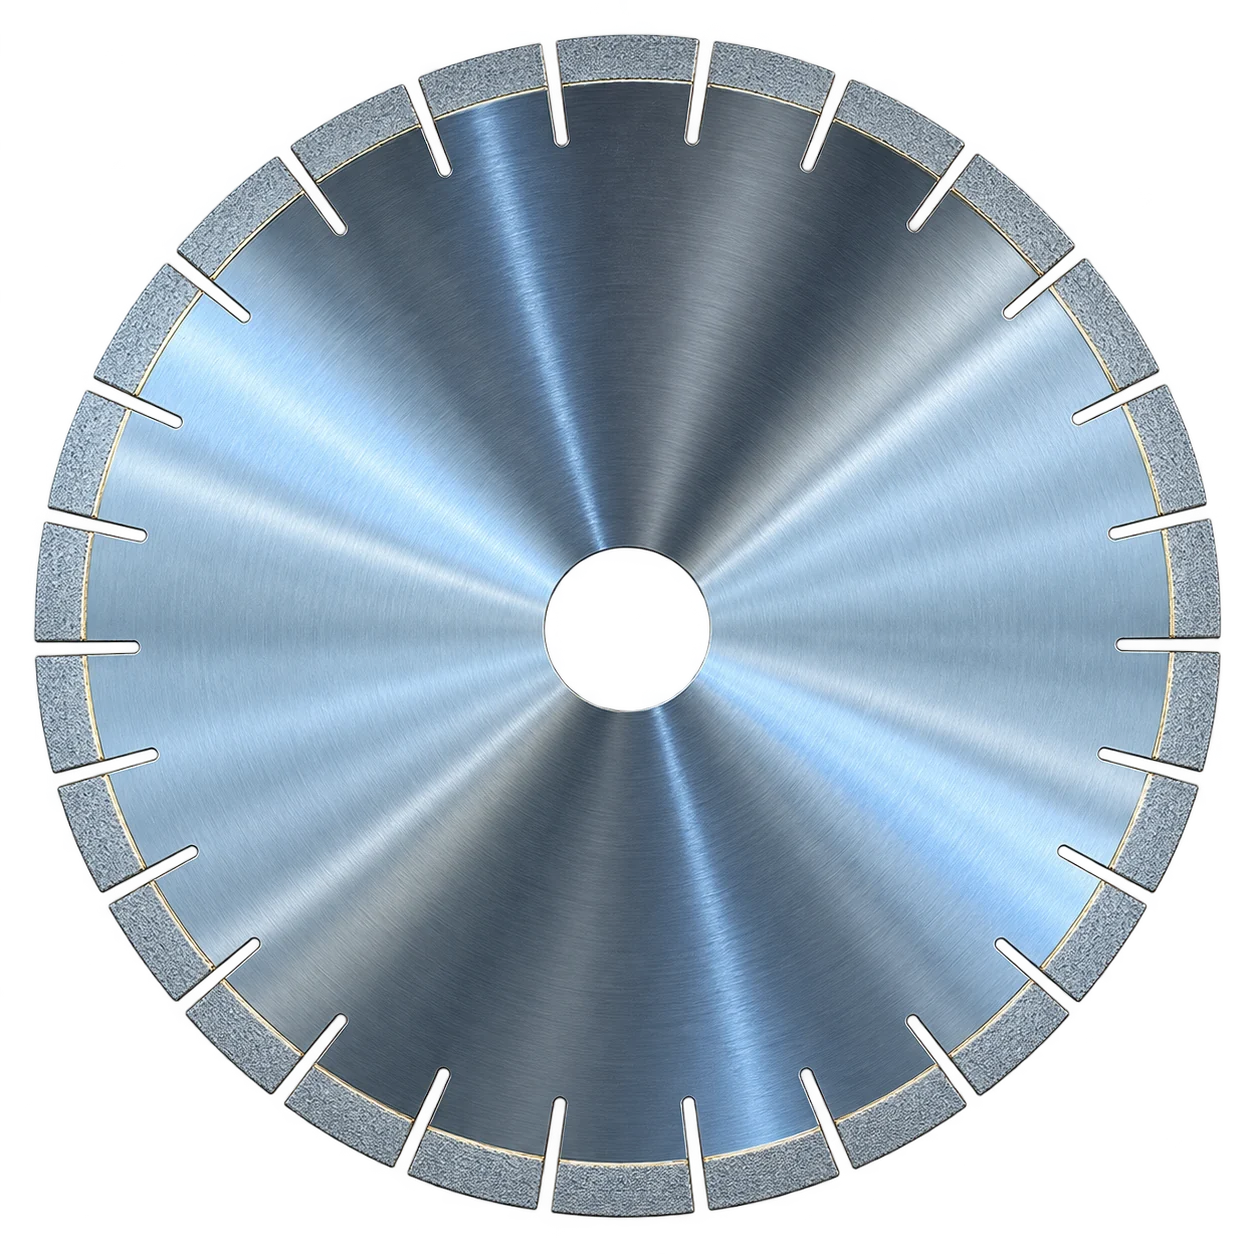
Diamond Blade For Granite (Stepped Segments / U-Slot)
Self-sharpening diamond matrix with stepped teeth design for hard, dense granite slabs.
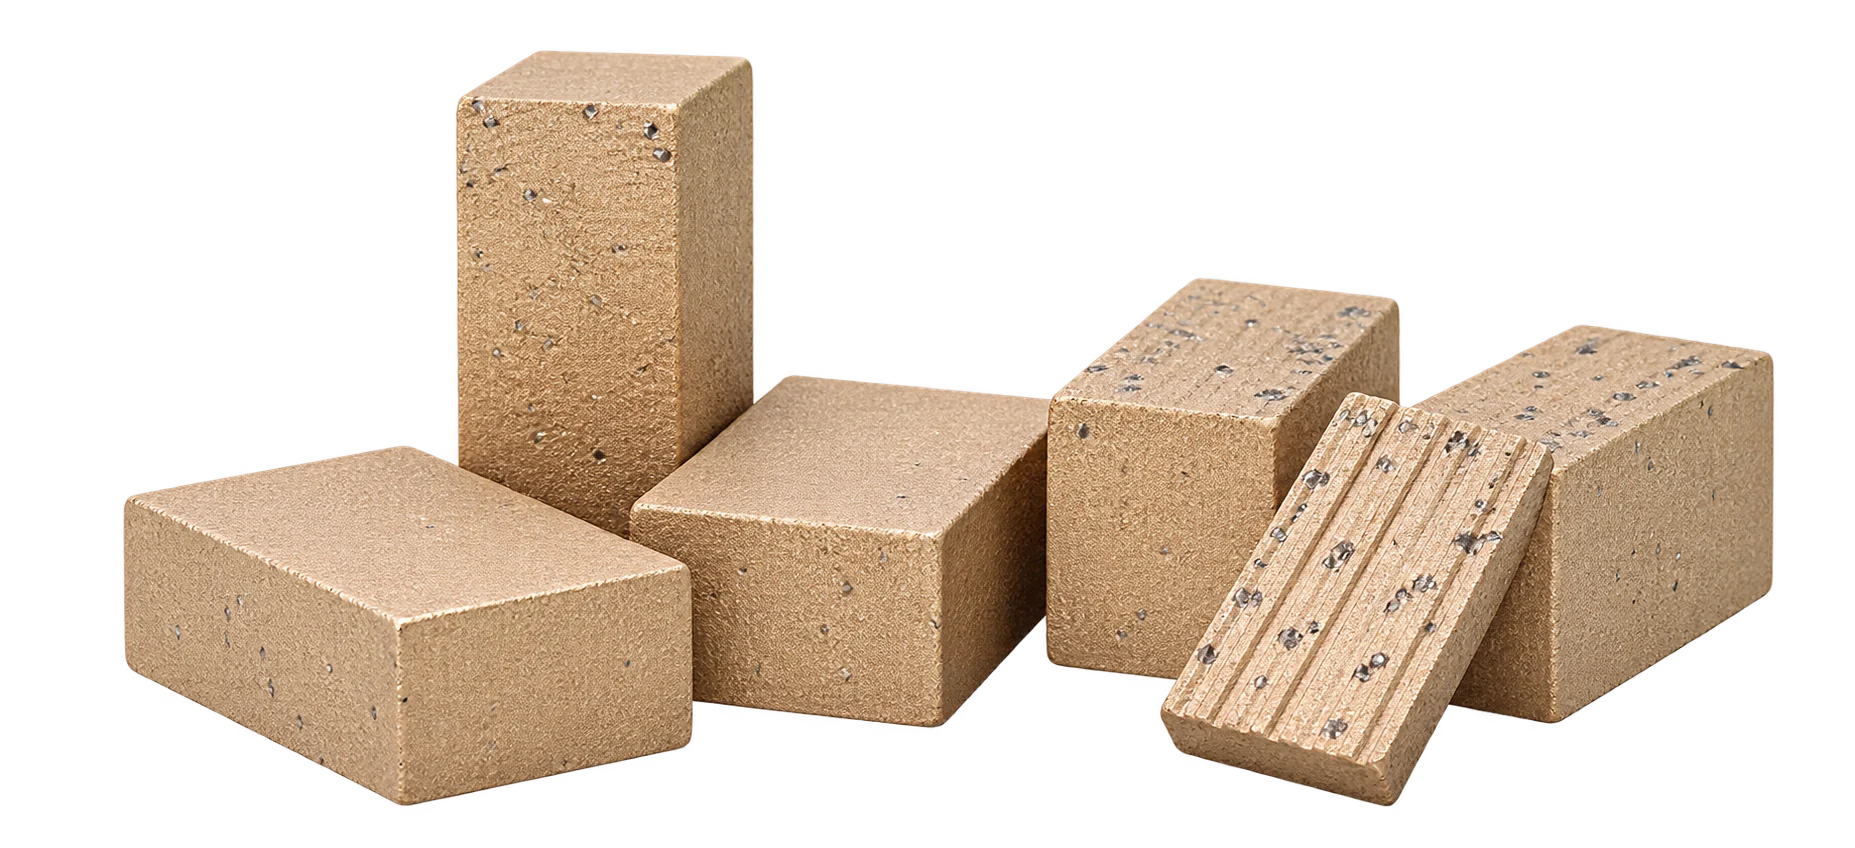
Marble Diamond Segments
High-quality raw materials with unique formula design. Stable quality and sharp cutting for marble discs.
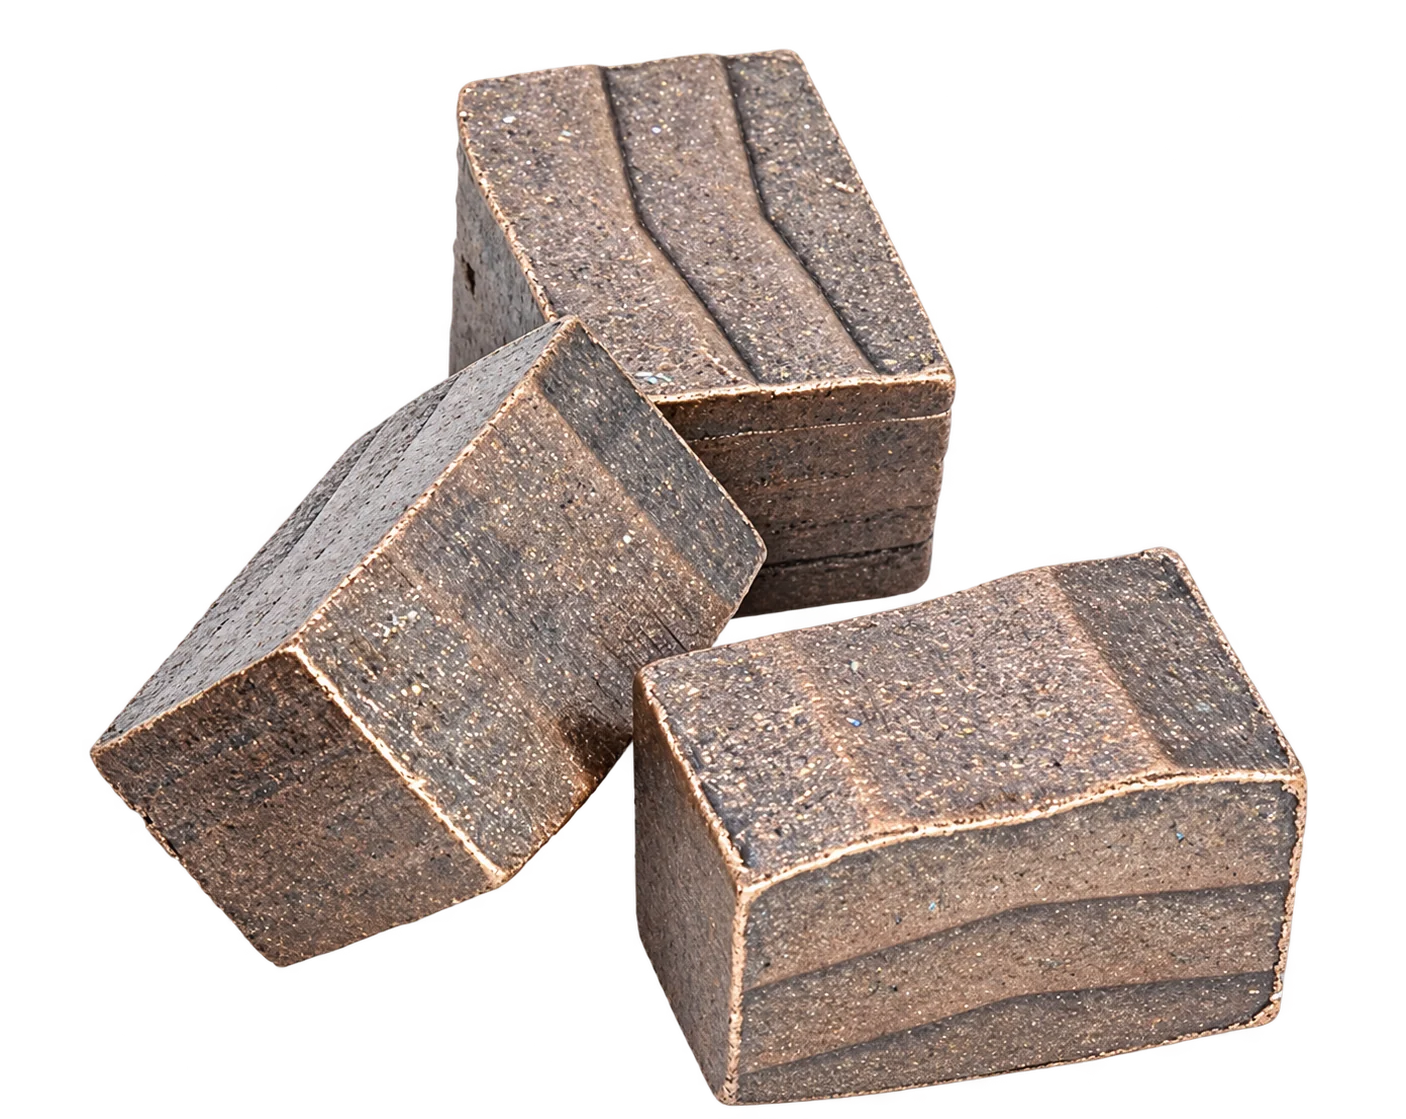
Granite Diamond Segments (Multi-Blade & Single Blade)
Unique matrix bond design, stable quality, sharp cutting, covering Φ1000mm to Φ2200mm block cutters.
Common Machining Bottlenecks & Engineered Remedies
Targeting real-world cutting and grinding challenges: edge chipping, floor tool glazing, block saw stalling, and OEM supply chain bottlenecks.
Edge Chipping & Corner Blowout on Sintered Stone Mitering
Micro-chipping and serrated spalling along cutlines or jagged 45° miter joints, causing high-value countertop slab rejections or tedious manual repairs.
Chipping may depend on the slab, blade condition, support, spindle runout, cooling, or feed. Record the defect location and check each factor.
- Check tool-marked maximum RPM and machine limits; record current peripheral speed
- Record straight and miter feed, then adjust in a trial against slab and machine guidance
- Inspect entry and exit chipping; adjust support and feed as needed
- Confirm coolant reaches the blade and workpiece contact zone
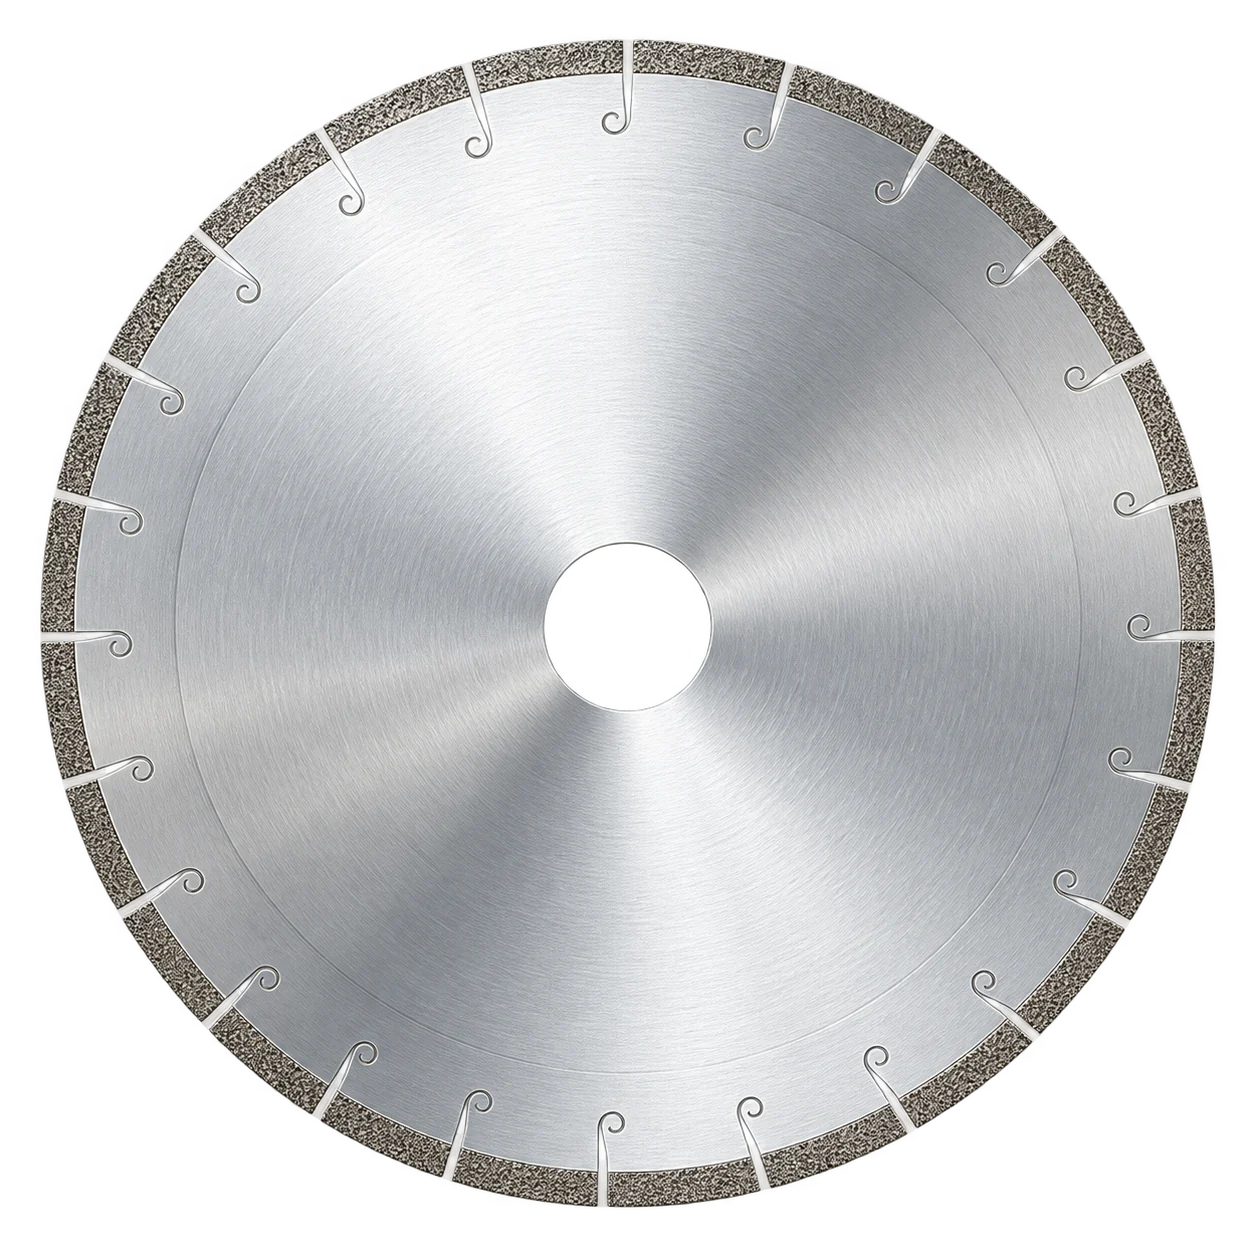
Diamond Blade For Dekton & Sintered Stone (J-Slot Silent)
Thin-segment blade listed for 3–20mm slabs; verify edge quality and wear in a trial cut on the target material.
Share your slab thickness, machine spindle RPM and power. We will review peripheral speeds and match trial specifications.